
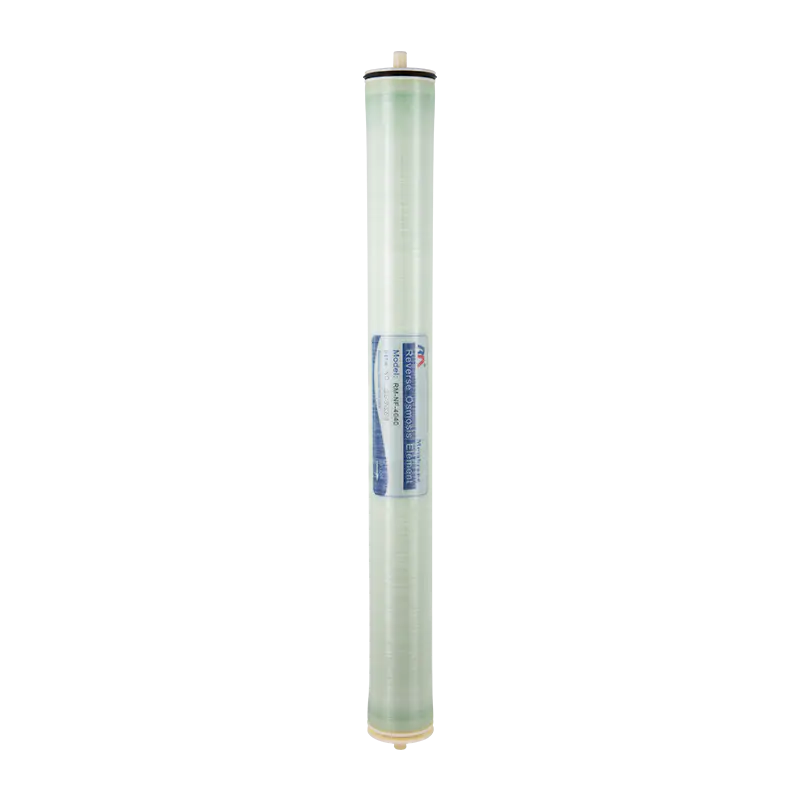
Advanced fluid purification processes rely heavily on sophisticated membrane structures to target specific dissolved contaminants within complex aqueous solutions. Industrial facility managers constantly seek innovative separation methods that balance high permeability with precise molecular selectivity. Nanofiltration water treatment has established itself as an essential intermediate technology bridging conventional ultrafiltration and high-pressure reverse osmosis systems. Engineers frequently select these specialized barriers to manage water softening, organic removal, and municipal supply purification efficiently.
The Core Scientific Principles of Nanofiltration
Porous separation barriers function by combining physical size exclusion mechanisms with complex electrostatic charge interactions across the membrane surface. Nanofiltration water treatment operates at lower hydraulic pressures compared to conventional reverse osmosis while retaining multivalent ions effectively. Specialized polymer compositions allow monovalent salts to pass through the barrier while selectively rejecting hardness-causing ions and micropollutants. This differential selectivity makes the technology valuable for specialized industrial separation tasks.
Proper design scopes and operating guidelines must be consulted in technical manuals to maintain optimal separation efficiency over time. Operators who fail to follow recommended manufacturer conditions risk compromising the structural integrity of installed filtration modules. Understanding fundamental rejection dynamics allows technical teams to maximize system performance across diverse commercial applications.
Understanding Water Yield Tolerance and Variations
System designers must account for manufacturing variations and flow tolerances when calculating total purification capacity for large facilities. The average water yield listed in technical documentation shows that individual element production errors remain within standard limits. Specifically, deviations for a single membrane element operating in series typically stay within a ten percent margin.
Minimum yields compared to nominal values across various series stay within twenty percent thresholds during standard operating periods. Plant operators utilize these performance metrics to predict system output accurately without experiencing unexpected hydraulic deficits. Accurate capacity planning prevents operational bottlenecks in municipal water treatment plants and industrial processing lines.
Storage Protocols and Preservation Solutions
Preserving delicate polymer structures prior to field installation requires strict adherence to standardized wet storage and packaging guidelines. Wet membrane components undergo rigorous factory testing before packaging in vacuum-sealed configurations filled with preservative solutions. Protective storage environments typically utilize a 1.0% sodium bisulfite solution to prevent biological growth during transit and warehousing stages.
Safe storage temperatures range strictly between four and forty-five degrees Celsius to prevent irreversible polymer degradation before deployment. Facility technicians inspect packaging integrity carefully upon delivery to verify that components have not suffered environmental exposure. Proper preservation safeguards active membrane surfaces until installation teams integrate them into operating systems.
Initial Operating Phases and Flushing Procedures
Initial system startup requires specific operational sequences to clear protective chemical residues from newly installed separation modules. Reverse osmosis and nanofiltration production water generated during the first hour of operation must be discharged safely. Bypassing initial permeate streams prevents residual storage chemicals from contaminating downstream industrial processes or municipal supply networks.
Technical operators monitor initial conductivity and pH levels closely to verify that rinse cycles achieve targeted baseline purity standards. Establishing proper hydraulic stabilization during the startup phase prevents premature scaling and surface fouling on sensitive polymer layers. Diligent adherence to commissioning protocols extends active membrane lifespans significantly.
Chemical Prohibitions and Additive Restrictions
Maintaining long-term membrane performance requires strict control over chemical additives introduced during storage, cleaning, and routine operation. Plant supervisors must prohibit any unauthorized chemicals that might interact adversely with sensitive composite polymer surfaces. Violating recommended chemical usage restrictions can cause severe structural damage and void manufacturer liability agreements entirely.
Technical guidelines require operators to consult certified engineering experts before introducing cleaning agents or experimental antiscalants into active flow loops. Strict adherence to chemical compatibility charts prevents accidental degradation of polyamide active layers and backing fabrics. Careful operational oversight protects financial investments in advanced filtration infrastructure.
Industrial Applications in Purification
Industrial manufacturing sectors depend on sophisticated separation techniques to prepare high-purity process water for sensitive production lines. Nanofiltration water treatment is widely applied in chemical manufacturing, pharmaceutical preparation, and beverage bottling plants worldwide. These systems remove natural organic matter and trace contaminants while preserving beneficial mineral balances where required.
Facility engineers integrate these versatile units into broader multi-stage purification trains to handle challenging feed water compositions. Tailoring separation stages to specific raw water profiles optimizes energy consumption and chemical usage simultaneously. Industrial processors achieve stringent quality benchmarks without incurring excessive operational expenditures.
Environmental Protection and Resource Recovery
Modern environmental regulations require industrial facilities to minimize wastewater discharge volumes through efficient internal recycling and reuse loops. Nanofiltration water treatment facilitates the concentration and recovery of valuable substances from complex industrial effluent streams. Processing saline wastewater streams helps plants comply with strict zero liquid discharge mandates while conserving regional water supplies.
Sustainable liquid management bridges the gap between industrial productivity and ecological conservation on a global scale. Environmental engineers rely on advanced membrane systems to reduce the ecological footprints of large-scale manufacturing operations. Effective recycling initiatives protect natural aquatic ecosystems from harmful chemical and mineral pollutant loads.
Conclusion
Industrial liquid management continues to evolve as global demand for clean resources intensifies across modern society. Runmo manufactures high-performance industrial filtration products designed to address rigorous separation challenges across diverse operational sectors. Runmo supplies specialized components optimized for advanced liquid purification, helping facility operators achieve sustainable outcomes. Contact the technical support department today to inquire about custom municipal filtration configurations for your facility.
